Engineered Industrial Pallet Racking Systems
Precision-fabricated Chinese heavy-duty storage solutions customized for commercial logistics hubs, cold storage chains, and distribution centers operating throughout Kenya.
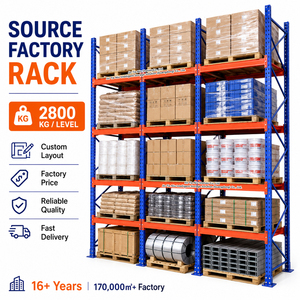
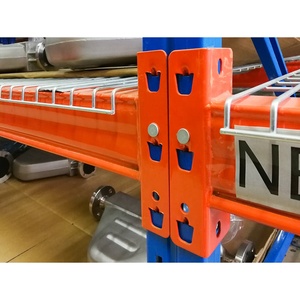
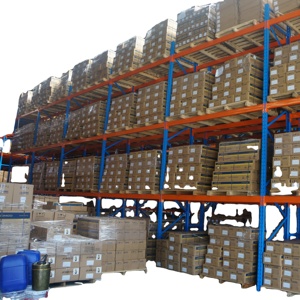
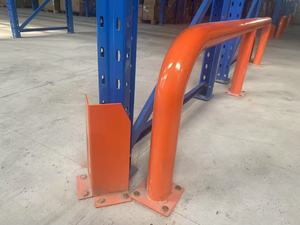
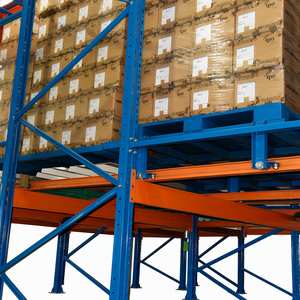
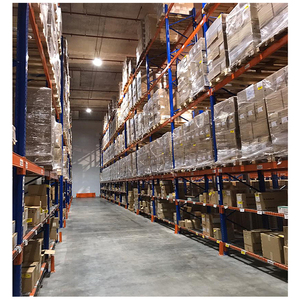
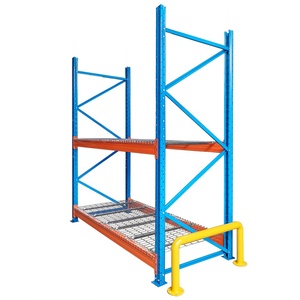
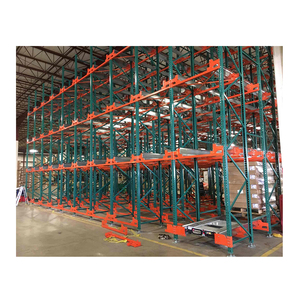
Industrial Racking Localization: Applications Across Kenya's Supply Chain Corridors
Kenya serves as the undisputed gateway to East and Central Africa, connecting international cargo routes from the Indian Ocean to landlocked markets in Uganda, Rwanda, South Sudan, and eastern DR Congo. With modern infrastructure advancements including the Standard Gauge Railway (SGR), the expansion of the Inland Container Depot Nairobi (ICDN) at Embakasi, and specialized industrial hubs such as the Tatu City Industrial Park and Africa Logistics Properties (ALP) North in Ruiru, supply chain operations demand industrial storage racks that maximize vertical cubic space while ensuring structural resilience under rigorous handling.
Selecting racking manufactured in China requires factoring in localized operational challenges distinct to the East African topography. From humidity resistance against Mombasa's maritime salt spray to geotechnical load dissipation across the Great Rift Valley's seismic fault zones, standard light-duty shelving systems fail under high-turnover cargo movements. Heavy-duty selective pallet racking, drive-in systems, and automated radio shuttle systems built to international RMI (ANSI MH16.1) and FEM 10.2.02 codes provide the exact high-yield load tolerance necessary for continuous 24/7 terminal operations.
Inland Container Depots (ICDN & Naivasha)
High-bay selective structural racks engineered for rapid SKU turnover, direct container deconsolidation, and seamless transfer from SGR freight trains to local distribution fleets.
Floriculture & Horticultural Cold Chains
Hot-dip galvanized and epoxy-finished drive-in and radio shuttle systems deployed in cold rooms near Jomo Kenyatta International Airport (JKIA) and Naivasha flower farms.
FMCG & Pharmaceutical Central Depots
Racking fitted with flanged wire mesh decking to support strict KEBS and WHO-compliant sanitary separation, overhead sprinkler penetrations, and clean inventory segregation.
Manufacturing Plants in Athi River & Thika
Heavy structural channel racking configured for raw steel coils, chemical drums, packaging pallets, and heavy spare parts, engineered with bolted impact-resistant uprights.
Cross-Border Wholesale & E-Commerce Depots
Multi-tier pick modules combining roll-formed pallet rack framing with integrated carton gravity flow lanes for rapid split-case sorting and regional parcel dispatch.
Kenya's Warehousing Trends: Modern Logistics & Vertical Optimization
Historically, warehousing in Kenya was dominated by single-story go-downs situated in Nairobi's Industrial Area along Enterprise and Commercial Roads. These low-ceiling structures relied on floor-stacking or primitive angle-iron shelving, which resulted in low volumetric utilization, high rate of pallet crush damage, and slow inventory retrieval. Over the past five years, the Kenyan logistics sector has witnessed a structural shift toward institutional-grade modern logistics parks, characterized by clear internal heights of 10 to 14 meters, laser-screeded flat floors compliant with FM2 standards, and broad column grids.
With prime warehousing rental rates in Nairobi averaging between $5.50 and $7.50 per square meter per month, warehouse operators and third-party logistics (3PL) providers can no longer afford to leave vertical airspace unutilized. Moving from a floor-stacked layout to a 5-level selective pallet rack immediately increases total storage capacity by 250% to 350% on the exact same footprint. Concurrently, regional logistics hubs in Kisumu—enhanced by Lake Victoria dry port developments—and Eldoret are embracing high-density drive-in and pallet flow racking to store agro-inputs, grain seeds, and regional commercial reserves.
Another major driver is the rapid adoption of reach trucks and Very Narrow Aisle (VNA) equipment in East Africa. As companies upgrade their forklift fleets from standard counterbalanced trucks to electric reach trucks capable of operating within 2.8-meter aisles, racking frames must feature tighter manufacturing tolerances, high-accuracy laser-cut beam connections, and robust base plate anchorage to withstand dynamic lateral oscillations.
Our Core Manufacturing & Engineering Advantages
Serving international contractors, warehouse developers, and local Kenyan procurement teams, our factory bridges advanced structural engineering with direct manufacturing scale. Operating state-of-the-art roll-forming mills, automated robotic welding cells, and fully automated powder coating lines, every component is manufactured to strict international specifications:
Certified Steel Traceability
Fabricated exclusively from premium Baosteel and Shougang Q235B and high-yield Q345B steel. Every production lot is delivered with complete metallurgical mill test certificates.
Automated Powder Coating
Multi-stage pre-treatment and automatic electrostatic powder curing lines ensure uniform 60-90 micron coating thickness, resistant to abrasion, chipping, and coastal salt corrosion.
Engineering & Seismic Design
Full CAD layout design and finite element analysis (FEA). Calculations verify beam deflection limits (≤ L/200), upright frame stability, and concrete slab anchorage under regional seismic forces.
Turnkey Export & PVoC Support
Complete export handling for Kenyan importers, including container nesting optimization, pre-export verification of conformity (PVoC), KEBS compliance documentation, and assembly guidance.
Kenya Procurement & Engineering FAQ
Critical considerations, clearing requirements, and technical answers for supply chain managers sourcing pallet racking from China for projects in Kenya.
How do we satisfy Kenya Bureau of Standards (KEBS) and PVoC requirements for imported racking?
What is the ocean transit time and container shipping route from China to Kenya?
How do your engineers design for Kenya's seismic activity and varied concrete slabs?
Can your racking systems accommodate both Euro pallets and standard industrial wood pallets?
How is on-site installation managed across industrial parks in Nairobi and Mombasa?
Optimize Your Facility with China's Premier Racking Manufacturer
Send your warehouse floor plans, ceiling clearance, and pallet specifications to our engineering team today for a complimentary CAD layout and detailed technical quote tailored to your Kenya project.
Send an Inquiry